Blog

  • What is GSM in Knitted Fabrics? and how to measure GSM?

    What is GSM in Knitted Fabrics? and how to measure GSM?

    Welcome back to Knitted Fabric.in! When you are sourcing, designing, or simply trying to understand the quality and weight of a textile, one term dominates the conversation: GSM. This metric is arguably the most crucial factor in determining how a knitted fabric will look, feel, and ultimately, how it will be used.


    Defining GSM

    GSM stands for Grams per Square Meter.

    • Grams (G): A unit of weight.
    • Square Meter (SM): A unit of area (1 meter X 1 meter).

    Simply put, the GSM of a fabric tells you the mass (weight) of the fabric if you cut it into a square meter section. It is a universal unit used across the textile industry to measure the density or substance of any fabric, whether woven or knitted.

    Why is GSM Crucial for Knitted Fabrics?

    For knitted fabrics, which are valued for their stretch and drape, GSM is more than just a weight measurement—it dictates the fabric’s practical use and performance:

    • End-Use Determination: The primary function of the fabric is defined by its GSM. For example, a low GSM jersey knit is perfect for summer T-shirts, while a high GSM fleece knit is required for winter jackets.
    • Costing and Pricing: Raw material cost is directly tied to weight. Higher GSM means more yarn was used per square meter, resulting in a higher cost for the fabric.
    • Handfeel and Drape: A lower GSM fabric is generally lighter, thinner, and drapes more loosely. A higher GSM fabric is thicker, heavier, and feels more substantial, often exhibiting better warmth and shape retention.
    • Opacity: Lower GSM fabrics (e.g., 100 GSM) are often sheer or semi-transparent, whereas higher GSM fabrics (e.g., 280 GSM) are opaque.

    GSM Ranges and Common Uses

    GSM is a sliding scale. Here is a general breakdown of how GSM ranges correspond to common knitted garments:

    GSM Range (Approximate)Fabric CharacteristicsTypical Knitted Product Uses
    80 – 130 GSMVery light, sheer, fine knit. Highly breathable.Inner linings, lightweight scarves, thin summer vests/camisoles.
    140 – 180 GSMLight to medium weight. Standard T-shirt quality.Summer T-shirts (jersey knit), lightweight polo shirts, everyday dresses.
    190 – 240 GSMMedium to heavy weight. Good opacity and structure.Quality polo shirts (pique), comfortable leggings, thicker long-sleeve T-shirts.
    250 – 350 GSMHeavy and substantial. Excellent warmth and durability.Sweatshirts (fleece, French terry), hoodies, jackets, heavy knitted joggers.
    360+ GSMVery heavy, dense knit. Maximum warmth and structure.Heavy winter coats, thick blankets/throws, specialized outerwear.

    How to Measure GSM Accurately

    Measuring GSM accurately requires precise tools and a standardized method to ensure the result is consistent and reliable. The fundamental principle is to weigh a small, precisely cut sample of the fabric and then scale that weight up to determine the weight of a full square meter.

    1. The Tools Required

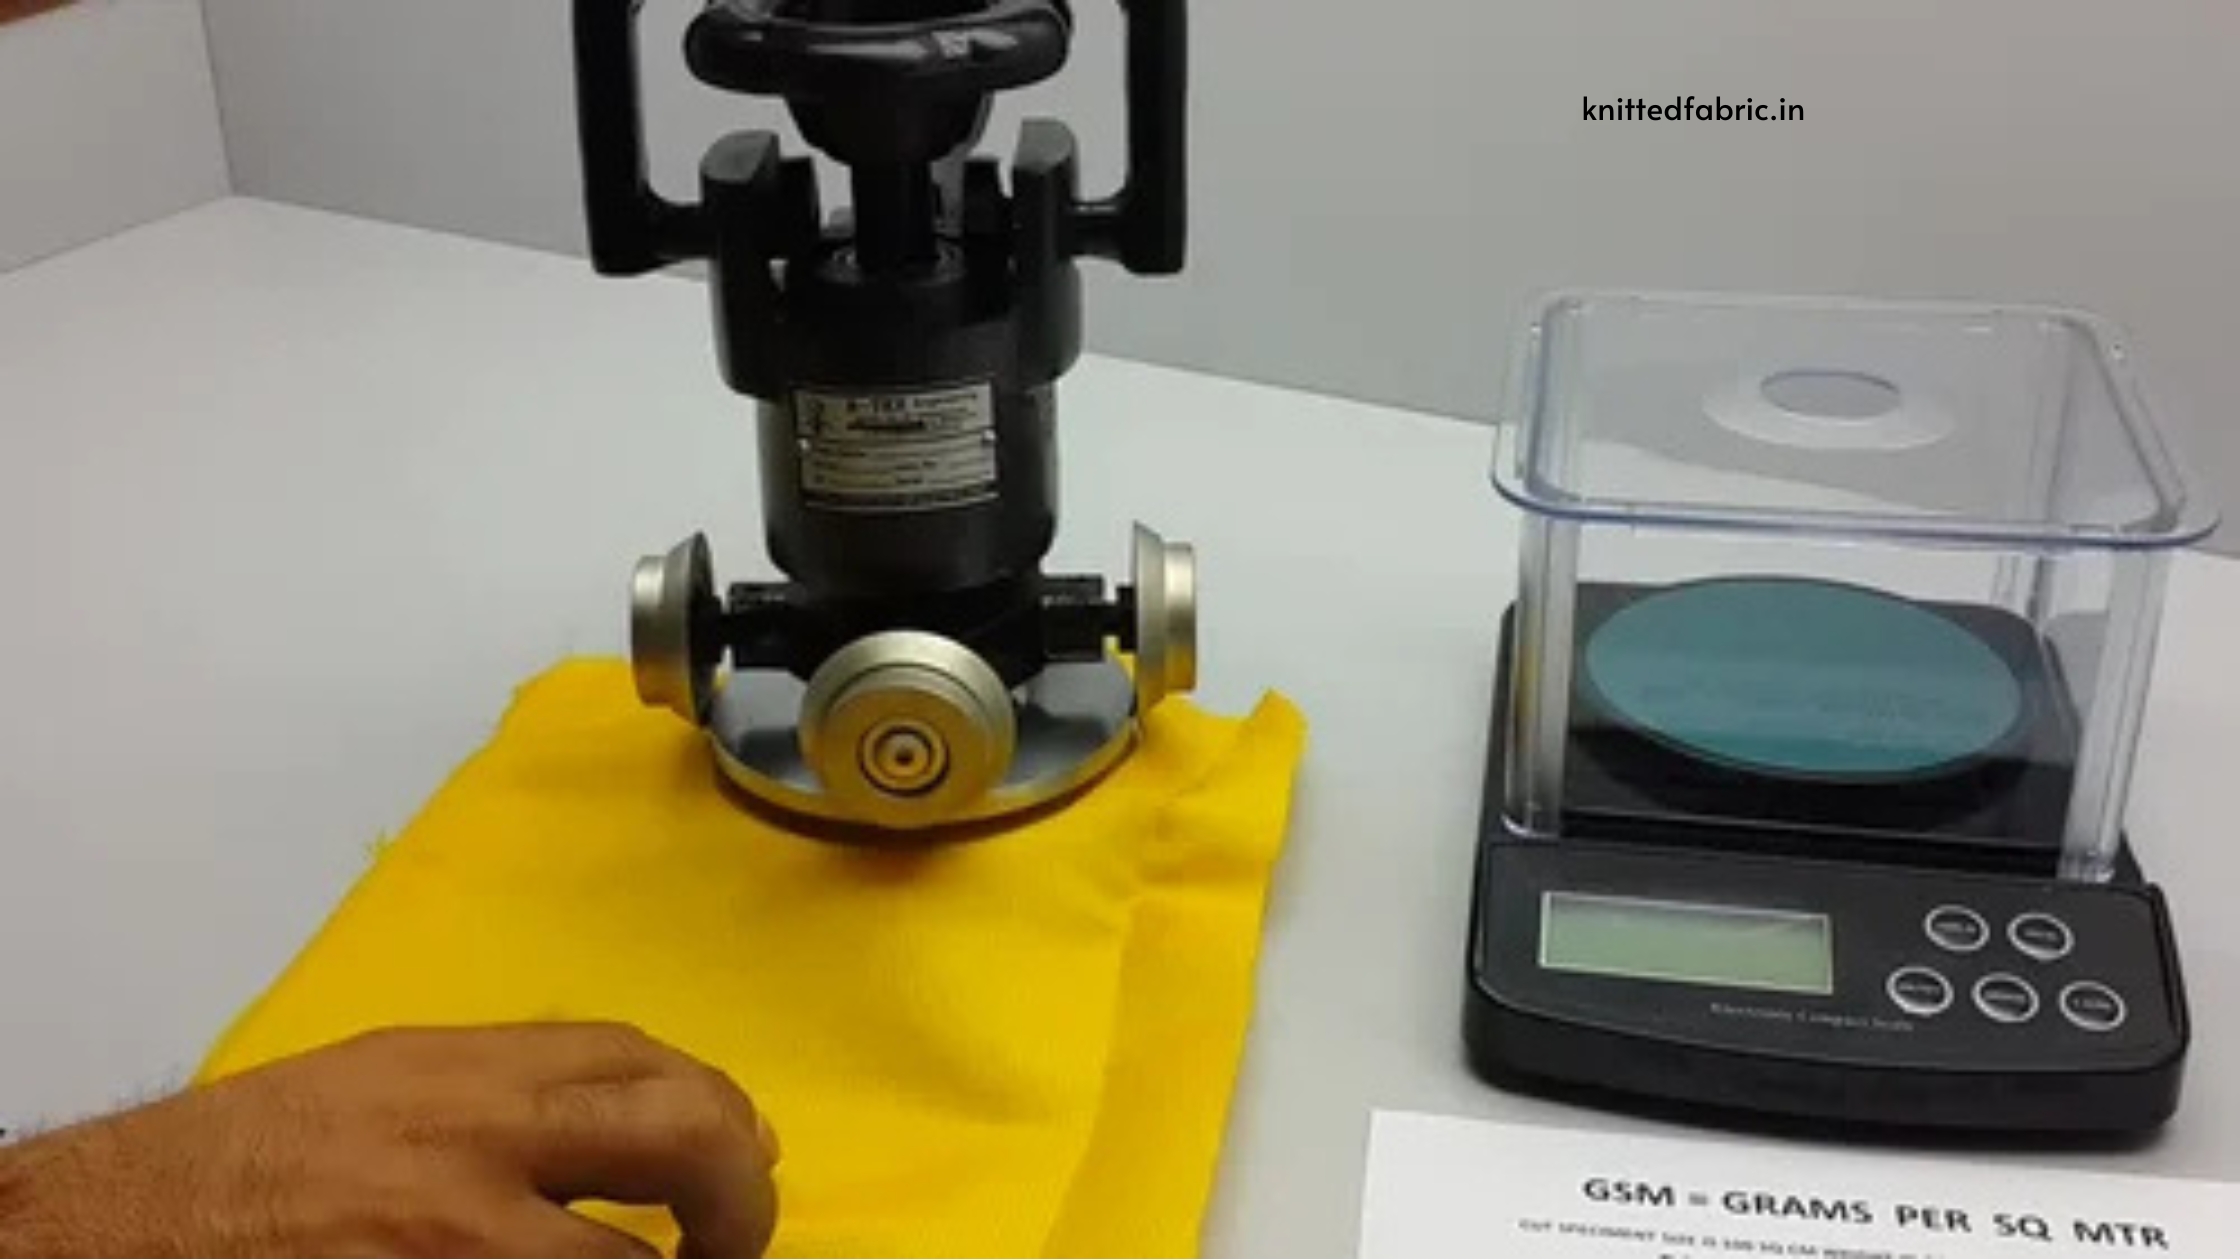
    • GSM Cutter (Circular Fabric Cutter): This specialized tool is essential. It is designed to cut a precise circular sample of fabric with a known area. This area is almost always 1/100th of a square meter (100 cm2).
    • Precision Digital Weighing Scale (Balance): This scale must be capable of measuring weight accurately to at least two decimal places (e.g., 0.01 grams).
    • Cutting Pad: A rubber or cork mat to protect the cutter blade and the surface underneath.

    2. The Step-by-Step Measurement Procedure

    Step A: Conditioning

    The fabric must be tested under standard atmospheric conditions (standard temperature and humidity, usually 20° C and 65% Relative Humidity). Moisture absorbed by the fabric can drastically affect its weight, so it’s critical to allow the fabric to “condition” (stabilize) in a controlled environment before testing.

    Step B: Cutting the Sample

    1. Place the fabric flat and wrinkle-free on the cutting pad.
    2. Place the GSM cutter firmly on the fabric.
    3. Press down and rotate the cutter’s handle to cut a perfect circular sample.
    4. Remove the sample carefully using tweezers (to avoid adding skin oil/moisture).

    Step C: Weighing and Calculation

    Since the standard GSM cutter cuts a sample that is 1/100th of a square meter (100 cm2):

    1. Weigh the cut fabric sample on the precision digital scale.
      Weight of Sample = W grams.
    2. The calculation is then straightforward: to find the weight of 1 square meter, you simply multiply the weight of the 1/100th square meter sample by 100.
      GSM = W X 100

    Example: If the cut sample weighs 1.85 grams, the GSM is 1.85 X 100 = 185 GSM.

    This method is widely used in calculating GSM of knitted fabrics that gives accurate result. It is easy to use and widely accepted in the knitting and textile industry. Some people also measure GSM by cutting the fabric into sqaure or rectangular shape that gives area measurement as 100 cm2.

    Understanding GSM allows you to compare fabric quality accurately and ensures you choose the perfect knitted fabric for your specific needs, whether it’s a light tee or a heavy fleece!
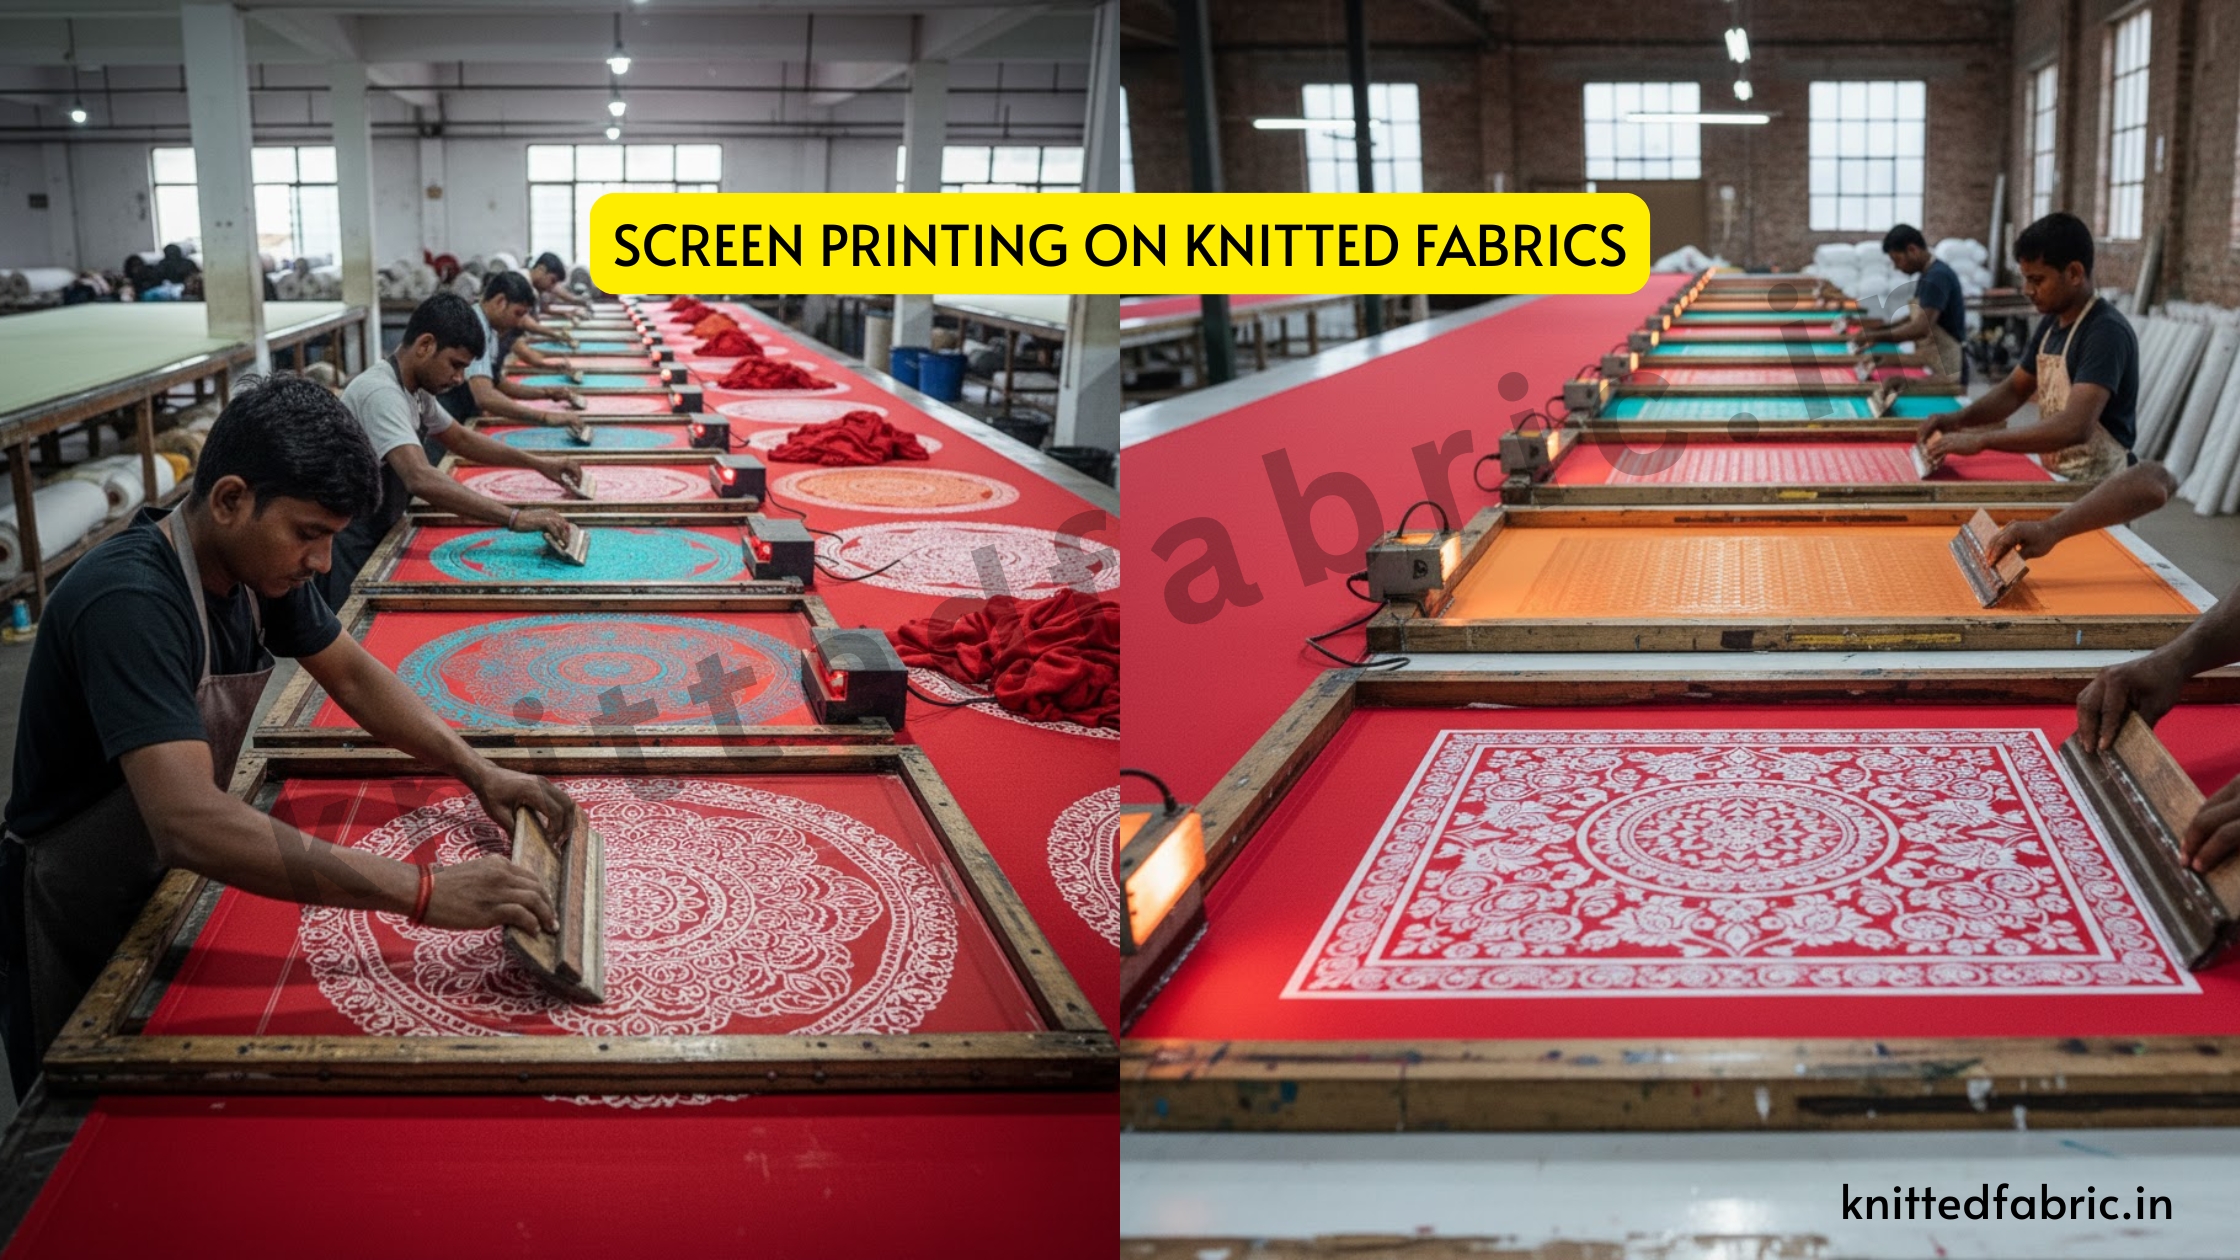
  • Screen Printing on Knitted Fabrics: Mastering the Art of Designs on Stretch

    Screen Printing on Knitted Fabrics: Mastering the Art of Designs on Stretch

    Welcome back to Knitted Fabric.in! In the world of textile decoration, screen printing stands as a classic and versatile technique, allowing for vibrant designs and intricate patterns on a wide array of fabrics. While it’s commonly associated with woven materials, screen printing on knitted fabrics is equally popular – just think of almost any graphic T-shirt or hoodie you own!

    However, working with the inherent stretch and unique texture of knits presents its own set of challenges and specialized techniques. For those of us keen on understanding how those striking designs appear on our favourite comfy garments, let’s dive deep into the art and science of screen printing on knitted fabrics.


    What is Screen Printing? A Quick Recap

    Before we talk about knits specifically, let’s briefly recap the screen printing process:

    Screen printing, also known as silk screen printing, is a stenciling method where ink is forced through a mesh screen onto a substrate (in our case, fabric).

    1. Screen Preparation: A mesh screen (traditionally silk, now often polyester) is stretched over a frame. A stencil of the design is created on this screen, blocking off areas where ink should not pass through.
    2. Placement: The fabric is laid flat on a printing platen (board).
    3. Ink Application: Ink is placed on the screen.
    4. Squeegee Action: A squeegee is used to pull the ink across the screen. This action forces the ink through the open (non-stenciled) areas of the mesh, directly onto the fabric below.
    5. Curing: The printed fabric is then sent through a dryer or heat press to cure the ink, making the design permanent and washable.

    This layered process allows for crisp designs and vibrant colours, with each colour in a multi-colour design requiring a separate screen.


    The Unique Challenges of Screen Printing on Knitted Fabrics

    Knitted fabrics, with their characteristic looped structure, behave very differently from stable woven fabrics. This stretchiness and texture introduce several considerations for screen printers:

    1. Stretch and Distortion: This is the biggest challenge. Knits inherently stretch. If the fabric stretches during printing, the design can become distorted, crack, or lose detail once the fabric relaxes.
    2. Fabric Instability: Knitted fabrics can move or shift on the platen more easily than wovens, leading to misregistration (colours not lining up correctly) or blurred prints.
    3. Ink Penetration and Coverage: The open, looped structure of some knits can cause ink to penetrate too deeply, bleeding through to the back, or result in patchy coverage if the ink isn’t optimized.
    4. Handfeel (Feel of the Print): Knits are prized for their softness and drape. A heavy, stiff print can ruin this, making the garment uncomfortable.
    5. Pilling: Rough inks or improper printing can sometimes exacerbate pilling on certain knitted fabrics, especially fleece.

    Mastering the Art: Techniques for Quality Screen Printing on Knits

    To achieve excellent results on knitted fabrics, printers employ specialized techniques and materials:

    1. Proper Fabric Tensioning:
      • Platen Adhesive: A strong but temporary adhesive (like spray tack or water-based adhesive) is crucial to hold the knit fabric firmly in place on the platen, preventing movement and stretch during printing.
      • Minimal Stretching: Operators must ensure the fabric is laid flat without being stretched. Laying it relaxed is key.
    2. Ink Selection is Crucial:
      • Plastisol Inks: These are widely used due to their opacity and vibrant colours. For knits, specialized soft-hand plastisol inks or low-bleed plastisols (for fabrics that tend to bleed dye into the ink) are preferred. They sit on top of the fabric.
      • Water-Based Inks (Discharge & Soft Hand): These inks penetrate the fabric more and become part of it, resulting in a much softer handfeel.
        • Discharge Inks: Remove the dye from a dark fabric and replace it with the ink’s pigment, creating an incredibly soft, vintage look. Best for 100% cotton knits.
        • Soft Hand Water-Based Inks: Designed for a natural feel, great for lighter fabrics.
      • Stretch Additives: For highly stretchy knits like rib, specific additives can be mixed into the ink to give it more elasticity, preventing cracking when the fabric stretches.
    3. Screen Mesh and Emulsion:
      • Lower Mesh Counts: Often, a slightly lower mesh count (e.g., 110-160 threads per inch) is used for printing on knits, especially for base layers, to allow more ink to pass through for good coverage on the textured surface.
      • Thicker Emulsion: A thicker layer of emulsion on the screen can create a larger ink deposit, helping to “fill” the valleys in the knit structure for a smoother print.
    4. Squeegee Technique:
      • Lower Pressure: Excessive squeegee pressure can push ink too deep into the fabric, causing bleed-through or reducing print crispness.
      • Proper Angle: A consistent squeegee angle ensures even ink deposit.
      • Flood Stroke: A “flood stroke” (gently pushing ink across the screen without downward pressure) helps fill the mesh openings before the print stroke, leading to better coverage.
    5. Flash Curing and Curing:
      • Flash Curing (Intermediate Drying): For multi-colour designs, a quick flash cure between colours stabilizes the previous layer, preventing smudging and ensuring clean registration for subsequent colours.
      • Thorough Curing: Proper final curing is essential. If the ink isn’t fully cured, it will wash out or crack easily. However, overheating can damage delicate knits. Temperature and dwell time must be precise.

    Popular Knitted Fabrics for Screen Printing

    While the techniques above allow printing on many knits, some are more common:

    • Cotton Jersey Fabric: The king of T-shirts! Excellent for screen printing with most ink types, offering good absorption and a classic look.
    • Cotton-Poly Blends (Jersey, Fleece): Offers a balance of cotton’s printability and polyester’s durability. Special attention to low-bleed inks might be needed to prevent dye migration from polyester.
    • French Terry Fabric: Popular for hoodies and sweatshirts, providing a good surface for designs.
    • Fleece Fabric: Can be screen printed, but often requires a thicker ink deposit and careful technique to achieve good coverage on its fuzzy surface, while maintaining a soft hand.

    Ensuring Quality: What to Look For

    When evaluating a screen-printed knitted garment, look for:

    • Smooth Handfeel: The print should feel soft and integrated with the fabric, not stiff or like a thick plastic layer.
    • No Cracking: The design should not crack when the fabric is gently stretched.
    • Sharp Edges: Lines and details should be crisp, not blurry or feathered.
    • Consistent Colour: The colour should be uniform across the entire design, without patches or unevenness.
    • No Bleed-Through: Ink should not visibly show through to the inside of the garment.

    Conclusion

    Screen printing on knitted fabrics is a highly skilled process that beautifully combines art and science. By understanding the unique properties of knits and employing specialized techniques, printers can transform a simple piece of fabric into a canvas for creative expression.

    So, the next time you admire a vibrant design on your favourite knitted T-shirt, you’ll know it’s not just ink on fabric, but a testament to precision, expertise, and a deep understanding of textile dynamics.

    Stay stylish and informed with Knitted Fabric.in!

  • How Circular Knitting Works: The Seamless Secret Behind Your Favourite Knits

    How Circular Knitting Works: The Seamless Secret Behind Your Favourite Knits

    Welcome back to Knitted Fabric.in! We’ve talked a lot about different types of knitted fabrics, their unique qualities, and how they’re finished. But have you ever wondered how many of your everyday knitwear items – from T-shirts and innerwear to socks and activewear – are made in a continuous, seamless tube? The answer lies in a fascinating process called circular knitting.

    Understanding the machinery behind the fabrics you love is incredibly insightful. Let’s pull back the curtain and explore the ingenious world of circular knitting.


    What is Circular Knitting?

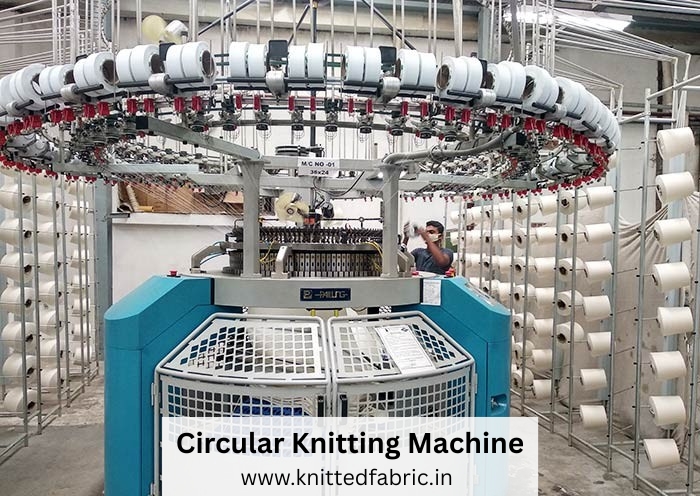
    At its simplest, circular knitting is a method of knitting fabric in a continuous, tubular form, without any seams. Unlike flatbed knitting machines that produce flat pieces of fabric (which then need to be cut and sewn together), circular knitting machines create a seamless “tube” of fabric, much like knitting a long sock or a continuous sleeve on large, round needles.

    This technique is incredibly efficient and is the backbone of mass production for many knitted garments worldwide, including a significant portion of the knitwear produced in India.

    Circular Knitting Machine diagram

    The Core Components of a Circular Knitting Machine

    To understand how it works, let’s look at the main parts of a typical circular knitting machine:

    1. Needle Cylinder: This is the heart of the machine. It’s a rotating cylinder (or sometimes a rotating cam box with stationary needles) that holds a large number of knitting needles arranged in a perfect circle.
    2. Needles: These are specialized latch needles (most common) or sometimes compound needles. Each needle moves independently up and down within its slot in the cylinder.
    3. Cams: These are stationary metal tracks that guide the needles’ movement. As the needle cylinder rotates, the needles ride up and down these cam tracks, performing the actions required to form loops.
    4. Yarn Feeders: These are mechanisms that supply yarn to the needles as they knit. A circular knitting machine can have multiple yarn feeders, allowing several courses (rows) of knitting to be formed simultaneously, dramatically increasing production speed.
    5. Sinkers: Small metal elements located between the needles. They assist in holding down the fabric loops as new loops are formed, ensuring consistent stitch formation.
    6. Fabric Take-down: Located below the knitting area, this system (usually rollers) gently pulls the newly formed fabric tube downwards, preventing it from bunching up and maintaining proper tension.

    How the Magic Happens: The Step-by-Step Process

    The process of circular knitting is a continuous dance of needles and yarn, forming loops one after another:

    1. Yarn Feeding: Yarn from cones is fed through tension guides to the yarn feeders, which present the yarn to the needles.
    2. Needle Movement – Raising: As the needle cylinder rotates, the cam tracks guide individual needles upwards. The hook of each needle rises above the old loop it’s holding, and the latch (a small movable part on the needle) opens up.
    3. Yarn Laying: The yarn feeder lays a new segment of yarn into the open hook of the raised needle.
    4. Needle Movement – Drawing Down: The cam then guides the needle downwards. As it descends, the old loop (which was held by the latch) slides up the needle stem and pushes the latch closed.
    5. Loop Formation: The newly laid yarn is pulled through the old loop. As the needle continues its downward movement, the old loop casts off, and the new loop is held securely by the needle’s hook.
    6. Fabric Take-down: The newly formed row of interlocked loops (a “course”) adds to the fabric tube, which is then gently pulled downwards by the take-down rollers.

    This entire sequence happens at incredible speeds, with hundreds or even thousands of needles working simultaneously to produce a seamless fabric tube. Because there are multiple yarn feeders around the circumference, several rows of knitting are being formed at any given moment, leading to very high production rates.


    Types of Circular Knitting Machines

    Circular knitting machines come in various configurations, each suited for different types of fabrics:

    • Single Jersey Machines: These machines have one set of needles and produce single-sided fabrics like the classic T-shirt material. They are very fast but the fabrics can curl at the edges and may be prone to spirality.
    • Double Jersey Machines (e.g., Rib, Interlock, Pique): These machines have two sets of needles (one in the cylinder and one in a dial above it). This allows them to create more complex, often reversible, and more stable fabrics like rib knits, interlocks, and pique. They are slower than single jersey machines but produce fabrics with better dimensional stability and less curl.
    • Jacquard Machines: These are advanced circular knitting machines that can create intricate patterns and designs by individually selecting needles to knit or miss stitches, allowing for complex fabric aesthetics.
    • Fleece Machines: Designed to produce fabrics like fleece and French terry, often with special attachments for brushing or loop creation.

    Advantages of Circular Knitting

    The widespread use of circular knitting stems from its numerous benefits:

    • High Production Speed: Multiple yarn feeders and continuous operation allow for very fast fabric production, crucial for meeting market demands.
    • Seamless Construction: Produces fabrics in a tubular form, eliminating side seams in garments like T-shirts, vests, and socks, which enhances comfort and reduces manufacturing steps (no need to sew side seams).
    • Cost-Effective: High output combined with reduced sewing needs can lead to lower production costs per metre or per garment.
    • Stretch and Comfort: The inherent nature of knitting creates stretchy, comfortable fabrics, which is further enhanced by the relaxed tubular process.
    • Versatility: Capable of producing a wide range of fabric types, weights, and structures (jersey, rib, interlock, fleece, etc.).

    The Role of Circular Knitting in Your Wardrobe

    Next time you pull on your favourite T-shirt, a comfy pair of track pants, or a seamless inner vest, take a moment to appreciate the unsung hero: the circular knitting machine. Its ability to rapidly produce high-quality, comfortable, and seamlessly structured fabrics is what makes so many of our everyday garments possible.

    Understanding these processes not only deepens your appreciation for textiles but also helps you make informed choices about the quality knitted fabrics you bring into your life.

    Stay curious and keep knitting with Knitted Fabric.in!

  • What is Tubetex Finishing in Knitted Fabrics? Unravelling a Key Process for Quality Knits

    Welcome back to KnittedFabric.in! Today, we’re diving into a crucial process in the world of knitted fabrics: Tubetex finishing. If you’ve ever wondered how your favourite knitted T-shirts, activewear, or innerwear get their perfect shape, consistent width, and smooth finish, Tubetex likely plays a significant role.

    For those of us keen on understanding and choosing quality knitted fabrics, knowing about finishing processes like Tubetex is key. It’s one of those behind-the-scenes steps that makes a huge difference in the final product you hold and wear.


    What is Tubetex Finishing? The Essence of Tubular Perfection

    Tubetex finishing refers to a specific type of textile finishing process applied primarily to tubular knitted fabrics. Unlike open-width fabrics that are cut and processed flat, tubular knits (like those made on circular knitting machines) remain in a continuous, seamless tube form throughout various stages.

    Tubular knitted fabric stock

    The Tubetex machine, or more broadly, the Tubetex process, is designed to handle these tubular fabrics. Its main objective is to:

    1. Dry the fabric evenly: After dyeing and washing, the fabric needs to be dried.
    2. Achieve uniform width: Knitted fabrics can shrink or stretch unevenly during wet processing. Tubetex helps set them to a consistent, desired width.
    3. Enhance fabric stability: It helps control shrinkage, reducing bowing (when courses run in a curve) and skewing (when courses are angled) for a stable fabric.
    4. Improve handfeel: The process can contribute to a smoother, softer feel.

    Think of it as a specialized ironing and drying system for tubular knits, ensuring they come out perfectly shaped and ready for cutting and sewing.


    The Tubetex Process: Step by Step

    The Tubetex finishing line typically involves several integrated stages, all designed for continuous, efficient processing of tubular knitted fabric:

    Knitted fabric finishing mechanism via TubeTex finishing machine
    1. Squeezing/Padding:
      • After dyeing or washing, the fabric, still in tubular form, first passes through a squeezing or padding unit. This removes excess water from the fabric using rollers, preparing it for drying and ensuring even moisture content. Sometimes, softening agents or other chemical finishes are applied here to enhance the fabric’s properties.
    2. Overfeeding and Spreading:
      • This is a critical step. The tubular fabric is “overfed” onto a set of spreading elements (often expanders or frames). This overfeeding mechanism ensures that the fabric is relaxed and not stretched too tightly lengthwise.
      • The spreading elements gently open the tubular fabric to the desired width. This is where width control is precisely managed. Operators can adjust the width according to the final garment requirements.
    3. Steaming/Heat Setting (Optional but Common):
      • Once spread to the correct width, the fabric might pass through a steaming zone. Steam helps relax the fibres and set the fabric in its desired state, crucial for dimensional stability and preventing future shrinkage. For synthetic blends, a heat-setting stage might be involved to permanently set the fabric’s dimensions.
    4. Drying:
      • The fabric then enters a drying chamber, usually a hot air dryer. The heated air removes the remaining moisture from the fabric. The speed of the fabric through the dryer and the temperature are carefully controlled to ensure even drying without over-drying or damaging the fibres.
    5. Compacting:
      • This is often the final and most important step for achieving shrinkage control and a soft handfeel. The fabric passes through a compacting unit, which uses a combination of steam, heat, and mechanical compression (usually felt blankets and rollers) to compress the fabric lengthwise.
      • This compression pushes the loops closer together, densifying the fabric and significantly reducing its potential for future shrinkage when washed by the consumer. This is particularly vital for cotton knits, which are prone to shrinking.
    6. Plaiting/Batching:
      • Finally, the finished, dried, and compacted tubular fabric is either plaited (folded) into trolleys or batched onto rolls, ready for the cutting department.
    TubeTex finishing process in action at Madhusudan Fabrics.

    Why is Tubetex Finishing So Important for Knitted Fabrics?

    Tubetex finishing offers several distinct advantages, making it indispensable for many knit manufacturers, especially for products like T-shirts, innerwear, and activewear:

    • Superior Dimensional Stability: This is perhaps the biggest benefit. By effectively compacting the fabric, Tubetex significantly reduces residual shrinkage, ensuring that your garments maintain their size and shape after wash. This is a key indicator of quality knitted fabric.
    • Uniform Width Control: It ensures that the fabric width is consistent throughout the roll, which is critical for efficient garment cutting and minimizing fabric waste.
    • Enhanced Handfeel and Drape: The relaxation, steaming, and compacting stages contribute to a softer, smoother fabric that drapes beautifully.
    • Reduced Spirality (Skewing): Knitted fabrics, especially single jersey, can have a tendency to twist or spiral after washing. Proper tension control and compacting in Tubetex finishing help minimize this issue, ensuring seams remain straight.
    • Seamless Garment Production: Since the fabric remains tubular, it’s ideal for producing seamless garments or garments with minimal side seams, common in items like hosiery, certain activewear, and innerwear.

    Applications of Tubetex Finished Knitted Fabrics

    You’ll find Tubetex finished fabrics used in a wide range of products, reflecting its importance in achieving consistent quality:

    • T-shirts and Polo Shirts: Ensures consistent fit and minimizes shrinkage.
    • Innerwear: Provides comfort, shape retention, and a smooth feel.
    • Activewear and Sportswear: Important for consistent stretch, recovery, and minimal shrinkage during intense use and washing.
    • Loungewear and Sleepwear: Delivers the desired softness and comfort.
    • Children’s Wear: Crucial for maintaining size and shape after frequent washes.

    The Bottom Line for Consumers and Manufacturers

    For manufacturers, investing in good Tubetex machinery and processes translates to higher quality products, fewer customer complaints about shrinkage or distortion, and more efficient production.

    For you, the consumer, a well-finished knitted fabric means:

    • Your favourite T-shirt will still fit perfectly after washing.
    • The seams on your knitted garment won’t twist awkwardly.
    • The fabric will feel consistently soft and comfortable against your skin.

    Next time you slip into a perfectly fitting, soft, and stable knitted garment, remember the intricate dance of fibres and machines, including the often-unsung hero: Tubetex finishing! It’s a testament to the technology that ensures the quality knitted fabric you love.

    Stay tuned to KnittedFabric.in for more insights into the fascinating world of knitted fabrics!

  • Stone Washed Knitted Fabric: Your Ultimate Guide to India’s Trending Softness & Style

    Stone Washed Knitted Fabric: Your Ultimate Guide to India’s Trending Softness & Style

    Are you on the hunt for comfortable, stylish, and uniquely textured fabrics? Look no further than stone washed knitted fabric! At Knitted Fabric.in, we’re all about helping you understand and choose the best quality knits, and this popular finish is a must-know for anyone interested in modern Indian fashion and textile trends.

    You’ve probably seen it everywhere – from your favourite comfy t-shirts and hoodies to stylish kurtas and activewear. That lovely faded, soft, and slightly vintage look often comes from the stone wash process. Let’s dive deep into what makes these knitted fabrics so special and why they’re a top choice for manufacturers and consumers across India.


    What Exactly is Stone Washed Knitted Fabric?

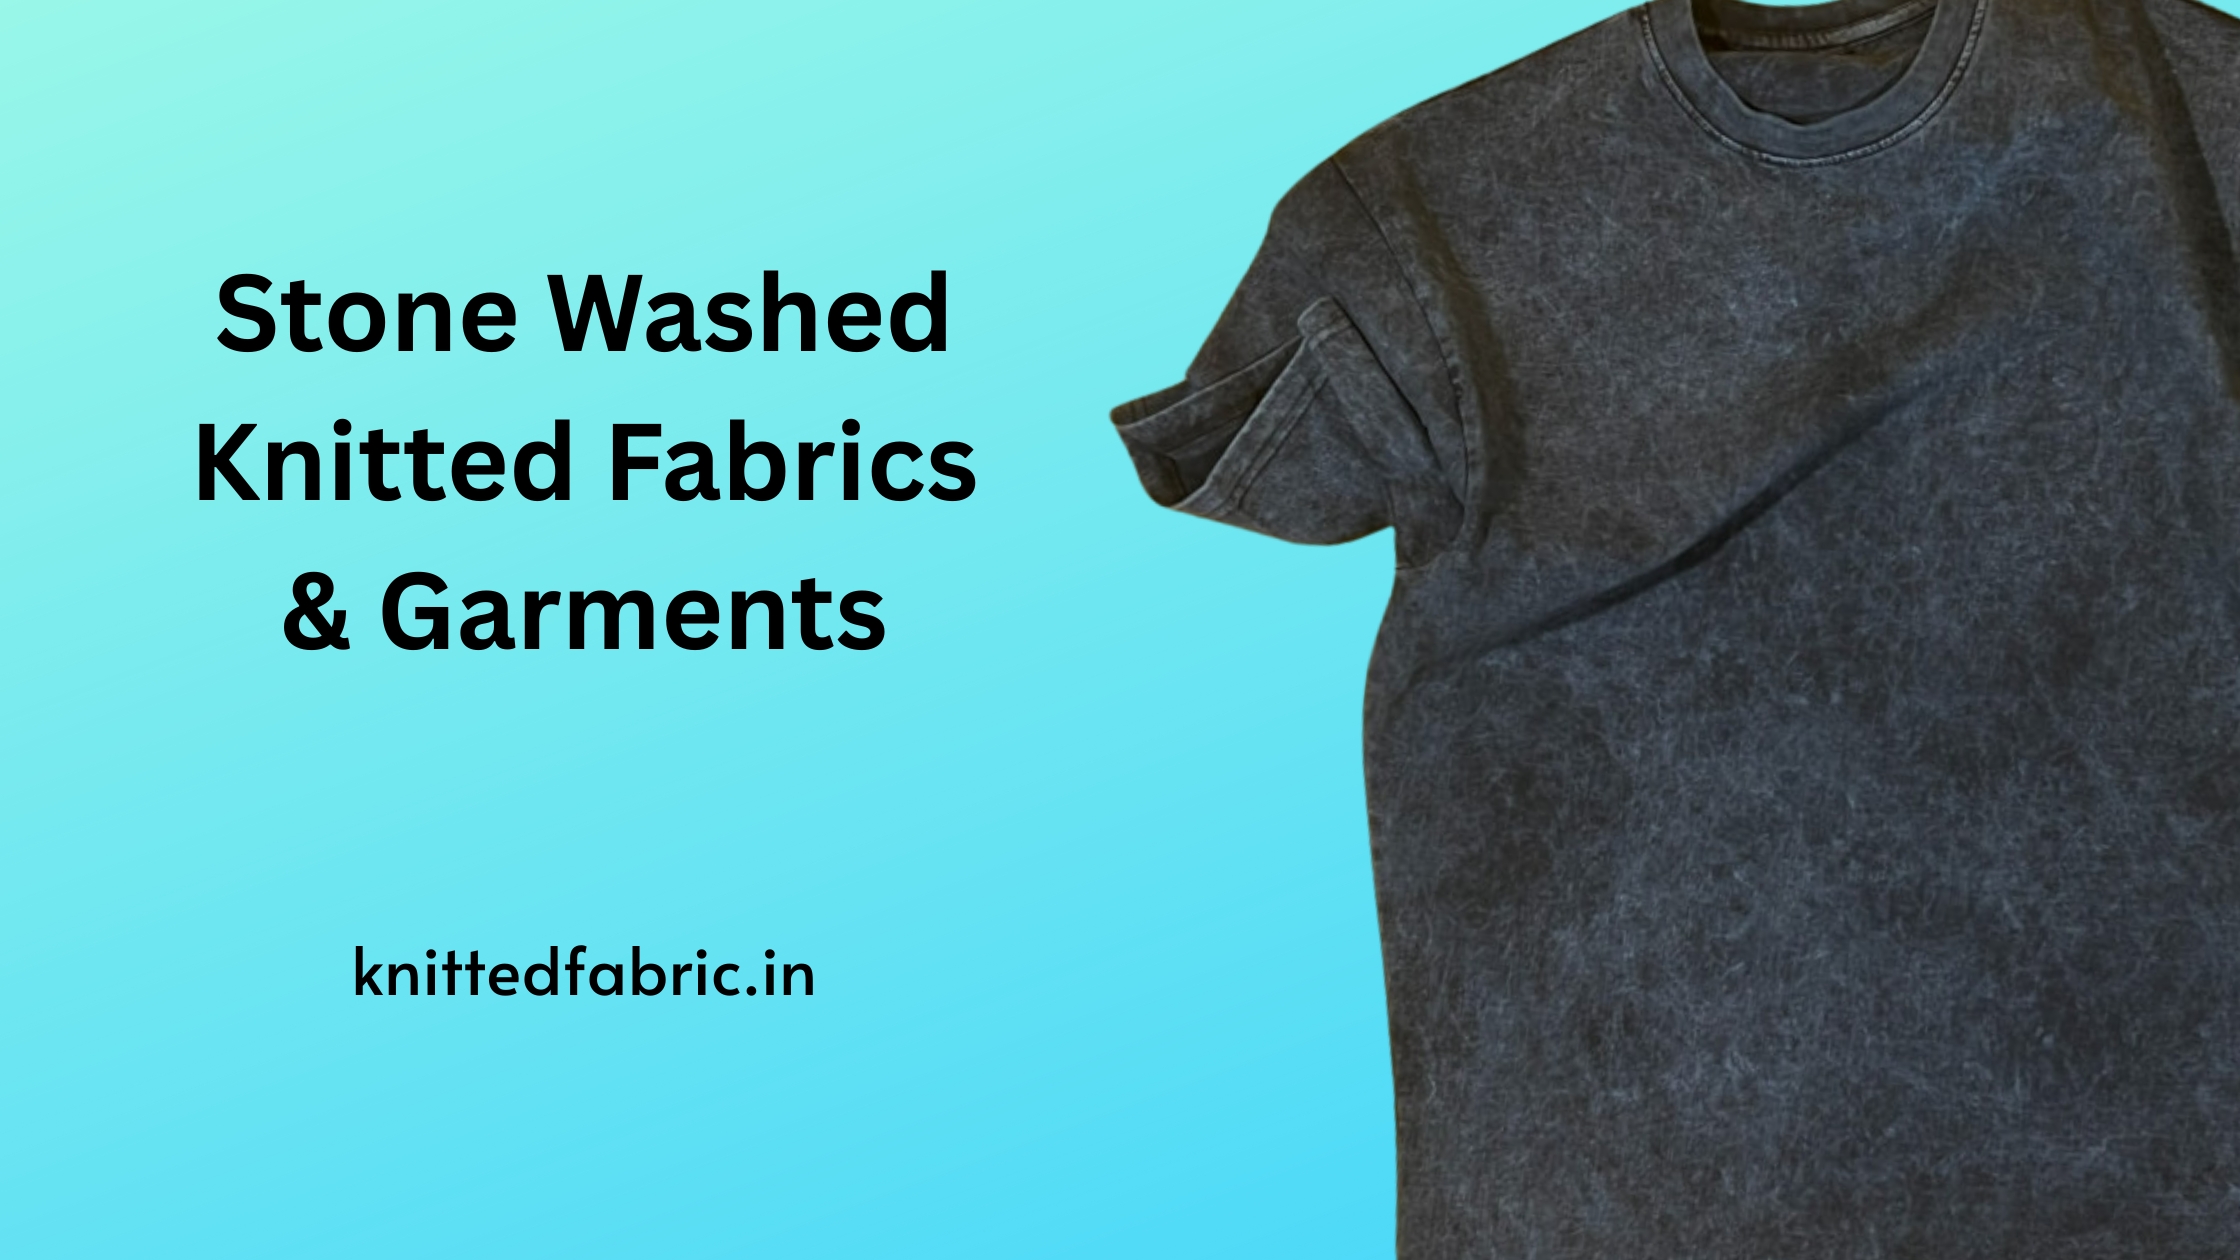
    Imagine your fabric going for a tumble with real stones! That’s the essence of stone washing. This textile finishing technique is designed to give knitted garments and fabrics a naturally faded, worn-in, and incredibly soft feel, just like your most cherished, old piece of clothing – but without the wait!

    The process involves washing the knitted material with large, abrasive stones (like pumice stone) in industrial washing machines. The friction created by the stones rubbing against the fabric and the machine walls gently breaks down the surface fibres. This action removes some of the dye, softening the material and giving it that desirable “distressed” or “aged” appearance.

    An image showing industrial stone washing machine for fabric in action

    The result? A fabric that is unbelievably soft, super comfortable, and has a subtly irregular, faded look. This can range from an even, gentle fade to a more pronounced, marbled effect, depending on the washing intensity and the original dye of the knitted fabric.


    Decoding “Acid Wash”: A Common Misconception

    Often, especially in India, you’ll hear the term “acid wash” used interchangeably with stone wash. While related, it’s important to clarify the difference. “Acid wash” became famous in the 1980s for its dramatic, high-contrast faded patterns, particularly on denim.

    However, true “acid washing” doesn’t use harsh acids. Instead, it typically involves:

    1. Treating pumice stones: These stones are soaked in a bleaching agent, commonly chlorine bleach or potassium permanganate.
    2. Tumbling with treated stones: As the fabric tumbles with these specially treated stones, the bleaching agent is randomly applied to the fabric’s surface.
    Acid washed tshirt and acid washed fabric
    Closup of Acid Washed Tshirt and Fabric

    This process removes dye in an uneven, patchy manner, creating those striking light or white areas against darker, unbleached portions. So, the “acid” in the common term refers to the strong, colour-removing action of the bleaching agent, not a literal acid.

    When used on knitted fabrics, this bleach-based process can create a unique cloudy, marled, or heavily faded effect, much more intense than a standard stone wash. The final look depends greatly on the knit structure (like jersey knit, fleece fabric), the fibre content (e.g., cotton knit fabric, blends), and the fabric’s initial dye colour.


    Why Is Stone Washed Knitted Fabric So Popular in India?

    There’s a reason why this finish is a hit in the Indian market. Here’s why stone washed knits are highly sought after:

    1. Ultimate Softness & Comfort: We Indians love our comfort! The rigorous washing breaks down any stiffness, making the fabric incredibly soft and comfortable right from day one. This “pre-loved” feel is a major draw.
    2. Unique Style Statement: Each stone-washed piece is unique, almost like a piece of art. The random fading and distressing create a distinct, vintage, and effortlessly cool look that makes you stand out. It’s perfect for a casual yet chic aesthetic.
    3. Evergreen Fashion Trend: These finishes regularly make a comeback in fashion circles. They offer a stylish nod to retro trends while staying relevant with contemporary designs, making them a versatile choice for your wardrobe.
    4. Better Fit & Feel: The intensive washing can help pre-shrink the fabric, leading to better size stability and less concern about shrinkage after home washes.
    5. Adds Texture and Depth: For plain fabrics, stone washing introduces visual texture and depth, transforming a simple knit into something much more interesting.

    Ideal Knitted Fabrics for Stone Washing & Acid Washing

    While many knits can be treated, some are particularly well-suited for these processes:

    • Cotton Knit Fabric (especially Jersey): A perennial favourite! Cotton’s natural absorbency and ability to become super soft make it ideal for stone washing. Think distressed t-shirts, comfortable dresses, and casual tops.
    • Cotton Fleece Fabric / French Terry Fabric: Perfect for achieving that vintage feel in your sweatshirts, hoodies, and joggers. The looped or brushed surface reacts beautifully to the distressing, creating a cosy yet stylish vibe. For example, Cotton RFD (Read For Dyeing) Fabric.
    • Cotton Blends: Knits blended with polyester or other synthetics can also be stone washed. The effect will primarily be seen on the cotton component, still offering a softened, worn look.
    • Knitted Denim Fabric: Yes, knitted fabrics can actually mimic the look and feel of denim! These are prime candidates for traditional stone washing to achieve a classic denim-like distressed appearance, but with the amazing stretch and comfort of a knit.

    Choosing and Caring for Your Stone Washed Knits

    To ensure you get the best out of your stone washed knitted fabric garments, consider these points:

    • Look for 100% Cotton: For the most dramatic and desirable “acid wash” effects, 100% cotton knitted fabrics are usually the best bet.
    • Fabric Weight: Heavier knits, like thick fleece, generally handle more aggressive washing well and often develop a richer, more textured distressed look.
    • Original Colour Matters: The initial dye colour plays a big role. Darker shades like indigo, black, or deep blues will show the most striking contrast when parts of the dye are removed.
    • Durability Check: While softening the fabric, the process can slightly reduce its strength. Always buy from reputable brands that balance style with garment longevity.
    • Follow Care Labels: Always, always check the wash care instructions on your garment. Stone-washed items might need specific washing to maintain their unique finish. Gentle cycles and cool water are usually recommended to prevent further fading or damage.

    Conclusion: Embrace the Lived-In Look!

    Stone washed knitted fabrics are more than just a passing fad in India; they represent a smart blend of textile innovation and contemporary fashion. They offer supreme softness, comfort, and a distinct visual appeal that makes each piece feel unique and personal. Whether it’s a casual tee, a cosy sweatshirt, or a trendy dress, a stone washed finish adds that special touch.

    Next time you’re shopping for comfortable and stylish clothing, remember the magic behind that effortlessly cool, “distressed” look. Understanding these processes helps you appreciate the craftsmanship and choose quality knitted fabrics that not only look smart but also feel fantastic and truly reflect your style.

    Stay tuned to Knitted Fabric.in for more valuable insights into the fascinating world of knitted fabrics!

  • What are Knitted Fabrics – Understand in Detail

    What are Knitted Fabrics – Understand in Detail

    At its core, a knitted fabric is a textile structure created by interlocking loops of yarn. Unlike woven fabrics, where two sets of threads (warp and weft) cross each other at right angles, knitting uses a single yarn (or multiple yarns) to form a series of connected loops. This unique loop structure is what gives knitted fabrics their distinctive properties.

    The Knitting Process: Forming Loops

    The fundamental unit of a knitted fabric is the loop, also called a stitch. The process involves forming new loops and pulling them through existing loops. This can be done manually with knitting needles (hand knitting) or, more commonly, on sophisticated knitting machines.

    Imagine a single yarn. In knitting, this yarn is bent into a loop. Then, another section of the same yarn (or a different yarn) is pulled through that first loop, forming a new loop. This process repeats, with each new loop interlocking with the previous one, creating a continuous fabric.

    • Course: A row of loops formed horizontally across the fabric.
    • Wale: A column of loops formed vertically along the length of the fabric.

    Key Characteristics of Knitted Fabrics

    The looped structure of knitted fabrics gives them several important characteristics:

    1. Elasticity and Stretch: This is the most defining feature. Because the yarn follows a meandering, looped path, knitted fabrics can stretch significantly in various directions (often in all four directions: lengthwise, crosswise, and on the bias). This makes them incredibly comfortable and form-fitting, allowing for freedom of movement.
    2. Drape: Knitted fabrics tend to drape beautifully, conforming to the body’s contours or falling softly. This is a result of their inherent flexibility.
    3. Softness: The looped construction generally makes knitted fabrics feel softer and less rigid than woven fabrics.
    4. Breathability: The open nature of the loops allows for good airflow, making many knitted fabrics breathable and comfortable to wear.
    5. Wrinkle Resistance: Knitted fabrics are generally less prone to wrinkling compared to woven fabrics because the loops can easily flex and return to their original shape.
    6. Insulation (Warmth): The spaces within the looped structure can trap air, providing good insulation and warmth, which is why knitted fabrics are popular for sweaters and winter wear.
    7. Run/Laddering Potential: A notable disadvantage of some knitted fabrics (especially weft knits) is their tendency to “run” or “ladder” if a loop is broken, as the continuous yarn can unravel.

    Types of Knitted Fabrics

    Knitted fabrics are broadly classified into two main categories based on how the loops are formed:

    1. Circular Knitting

    • How it works: In circular knitting, loops are formed horizontally across the fabric using a single yarn (or multiple yarns at different feeders). Think of hand knitting – you’re essentially doing circular or weft knitting.
    A functional circular knitting machine
    A functional Circular Knitting Machine
    • Characteristics:
      • Highly stretchy and elastic.
      • Softer and more pliable.
      • Can unravel easily if a yarn breaks (prone to runs).
      • Can be made on flat or circular knitting machines.
    • Common Types of Weft Knits:
      • Jersey Knit (Plain Knit/Single Knit): The most common type. It has a distinct “V” pattern on the front (technical face) and horizontal loops (purl stitches) on the back (technical back). It curls easily at the edges when cut. Used for T-shirts, dresses, underwear.
      • Rib Knit: Characterized by visible vertical ribs on both sides, created by alternating knit and purl stitches in the same row. Offers excellent crosswise stretch and recovery. Used for cuffs, collars, waistbands, and fitted garments.
      • Interlock Knit: A type of double knit that looks like two jersey fabrics knitted together. Both sides appear identical with a smooth, lengthwise ribbed texture. It’s thicker, more stable, and less stretchy than single jersey, with good shape retention. Used for polo shirts, dresses, and activewear.
      • Purl Knit: Has a textured, bumpy surface on both sides, making it reversible. It has good lengthwise and crosswise stretch but is less common due to slower production. Often used for sweaters and scarves.
      • French Terry: A knit fabric with loops on one side (usually the inside for absorbency) and a smooth surface on the other. Popular for sweatshirts and casual wear.
      • Fleece: A brushed knit fabric (often originally jersey or French terry) that has a soft, fuzzy pile on one or both sides for warmth.

    2. Warp Knitting

    • How it works: In warp knitting, multiple yarns are used, with each yarn having its own needle. Loops are formed vertically along the length of the fabric in a zigzag or diagonal pattern.
    A Warp Knitting Machine
    A Warp Knitting Machine
    • Characteristics:
      • Less stretchy than circular knits, but still elastic.
      • More stable and run-resistant (less likely to unravel if a yarn breaks).
      • Often produces denser fabrics.
      • Generally produced at higher speeds on specialized machines.
    • Common Types of Warp Knits:
      • Tricot: A very common warp knit with lengthwise ribs on the front and crosswise ribs on the back. It’s smooth, lightweight, and durable. Used for lingerie, swimwear, athletic wear linings, and automotive interiors.
      • Raschel: This type of warp knit can produce a wide range of fabrics, from fine laces and mesh to heavy carpets and industrial textiles. It often features openwork designs and intricate patterns.
      • Milanese Knit: Known for its fine diagonal rib pattern on the face and a diagonal structure on the reverse. It’s lightweight, soft, and run-resistant, often used for gloves and apparel where a smooth, flowing drape is desired.

    Applications of Knitted Fabrics

    Due to their versatility and unique properties, knitted fabrics are used in a vast array of products:

    • Apparel: T-shirts, sweaters, dresses, leggings, activewear, hosiery, socks, underwear, swimwear, hats, scarves.
    • Home Textiles: Blankets, throws, upholstery, curtains (some types).
    • Technical Textiles: Medical bandages, protective gear, automotive textiles, geotextiles.

    Understanding the differences between knitted and woven fabrics, and the various types of knits, is crucial for anyone involved in textile production, design, or even just choosing quality fabrics for personal use.